EN
RU
中文
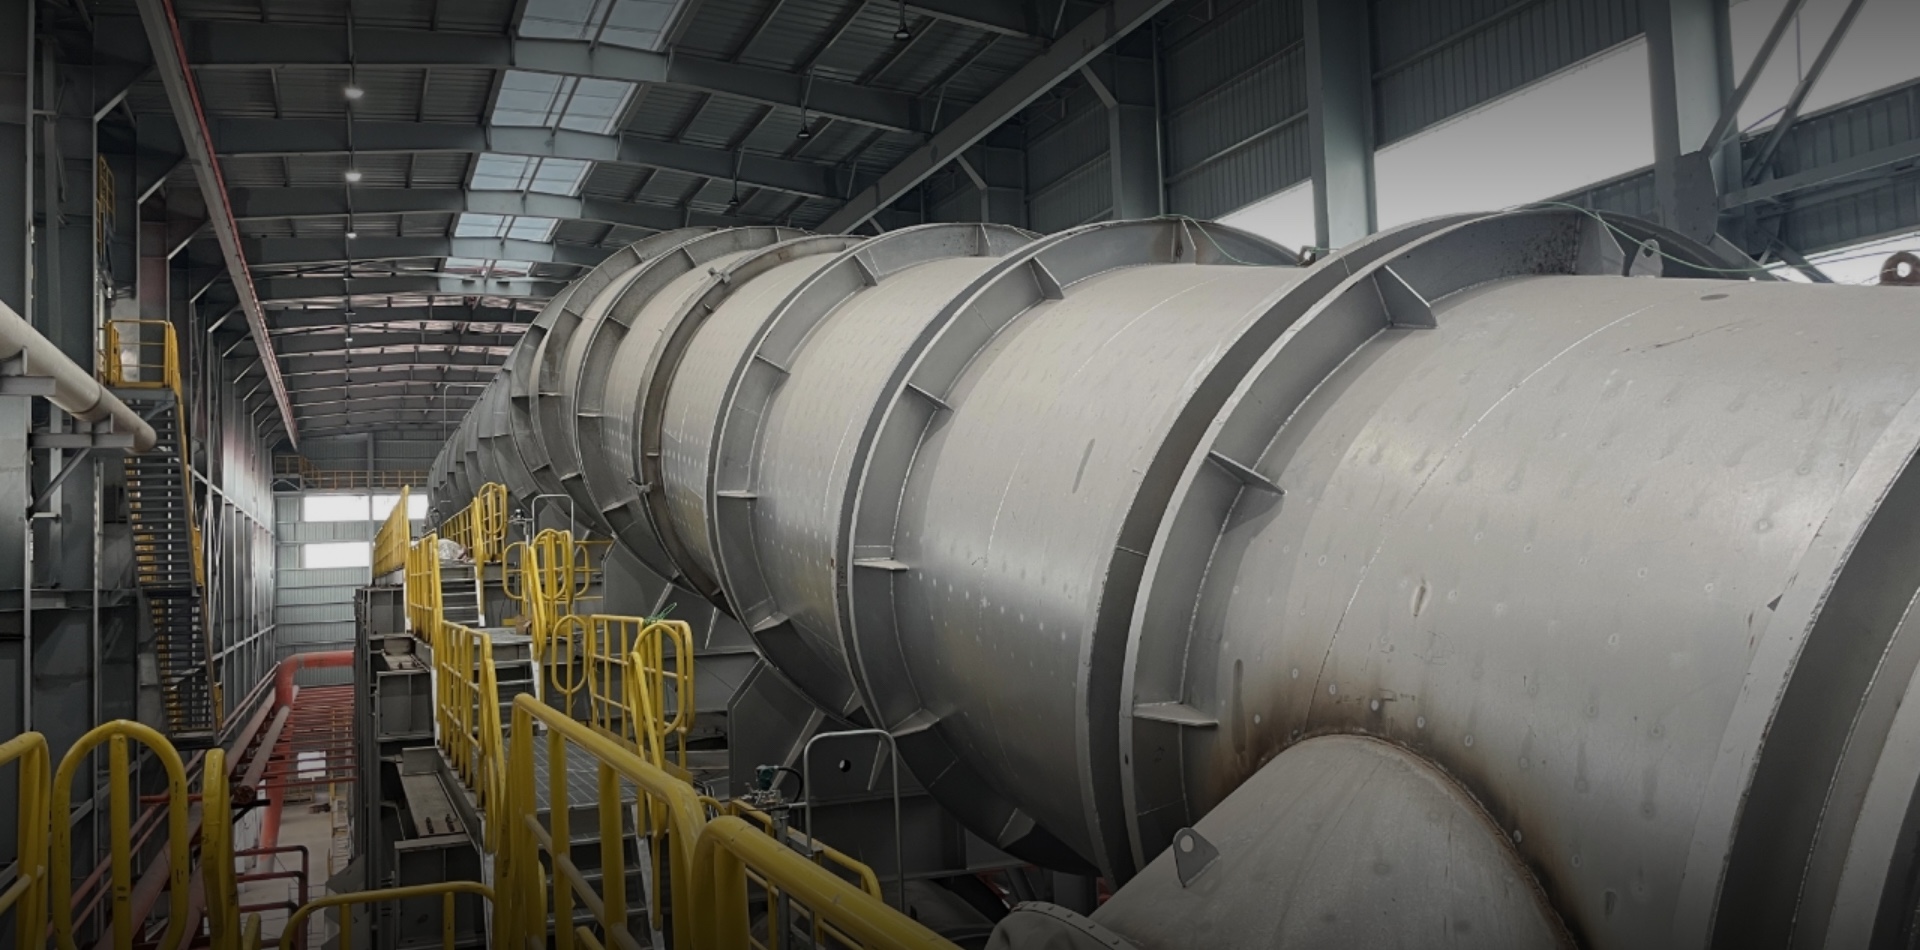

Automatic Pelletizing Scene
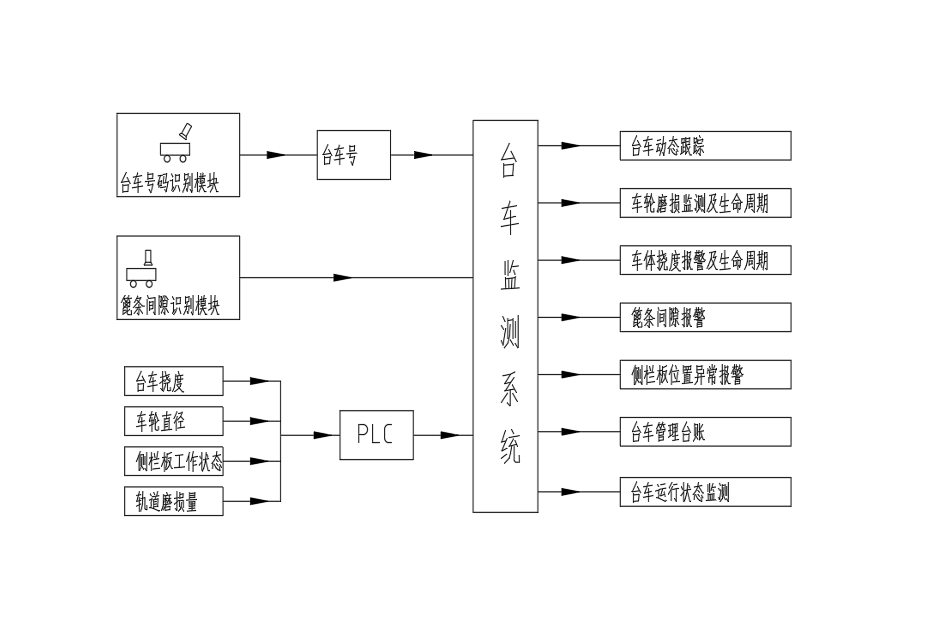
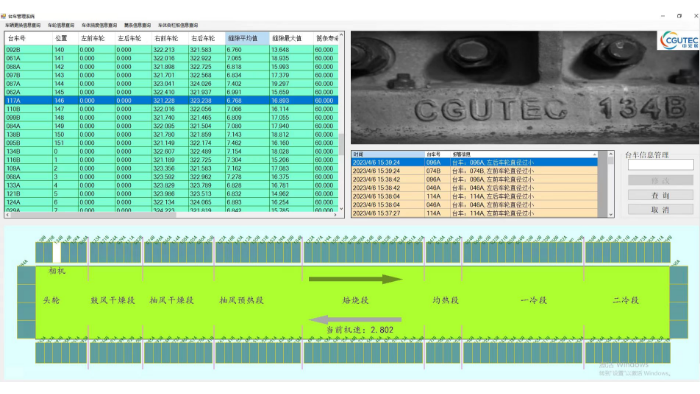
Trolley Monitoring System Architecture
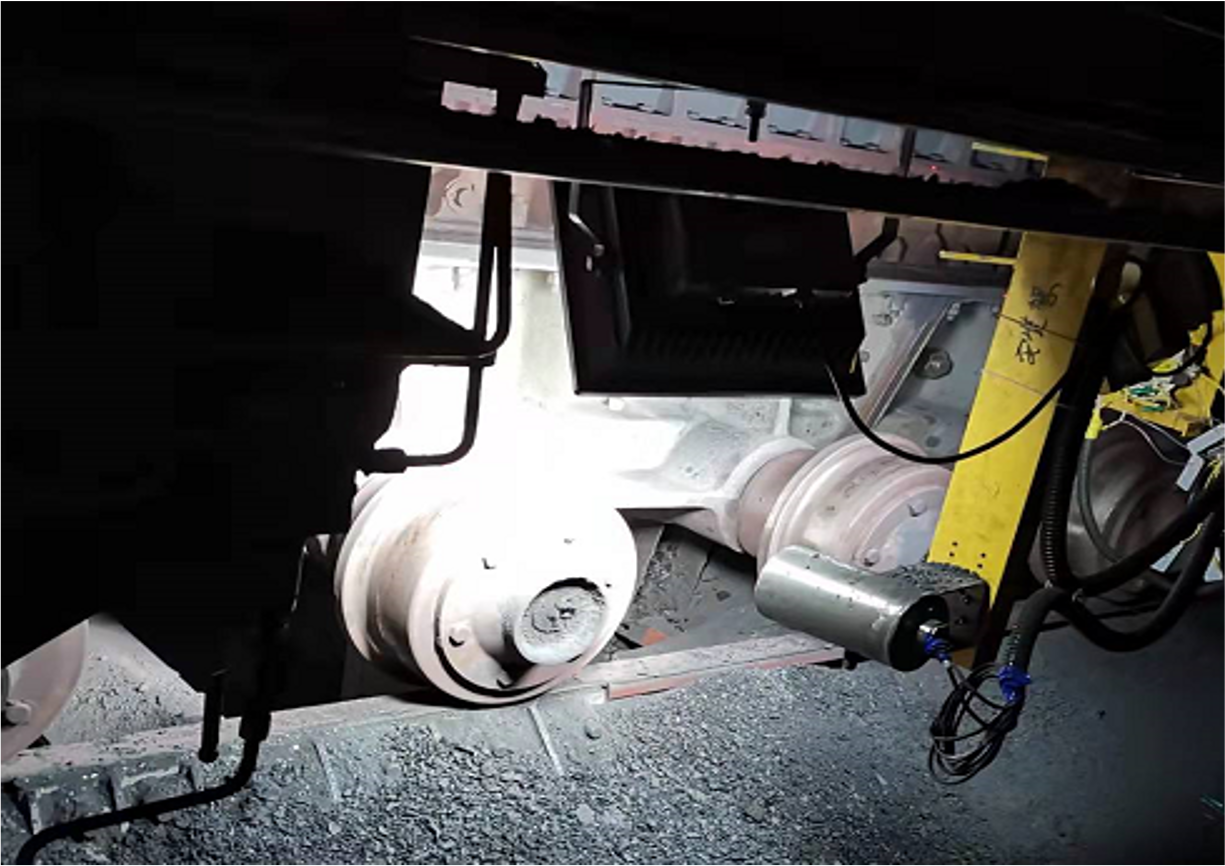
On-site Photo of Trolley Monitoring
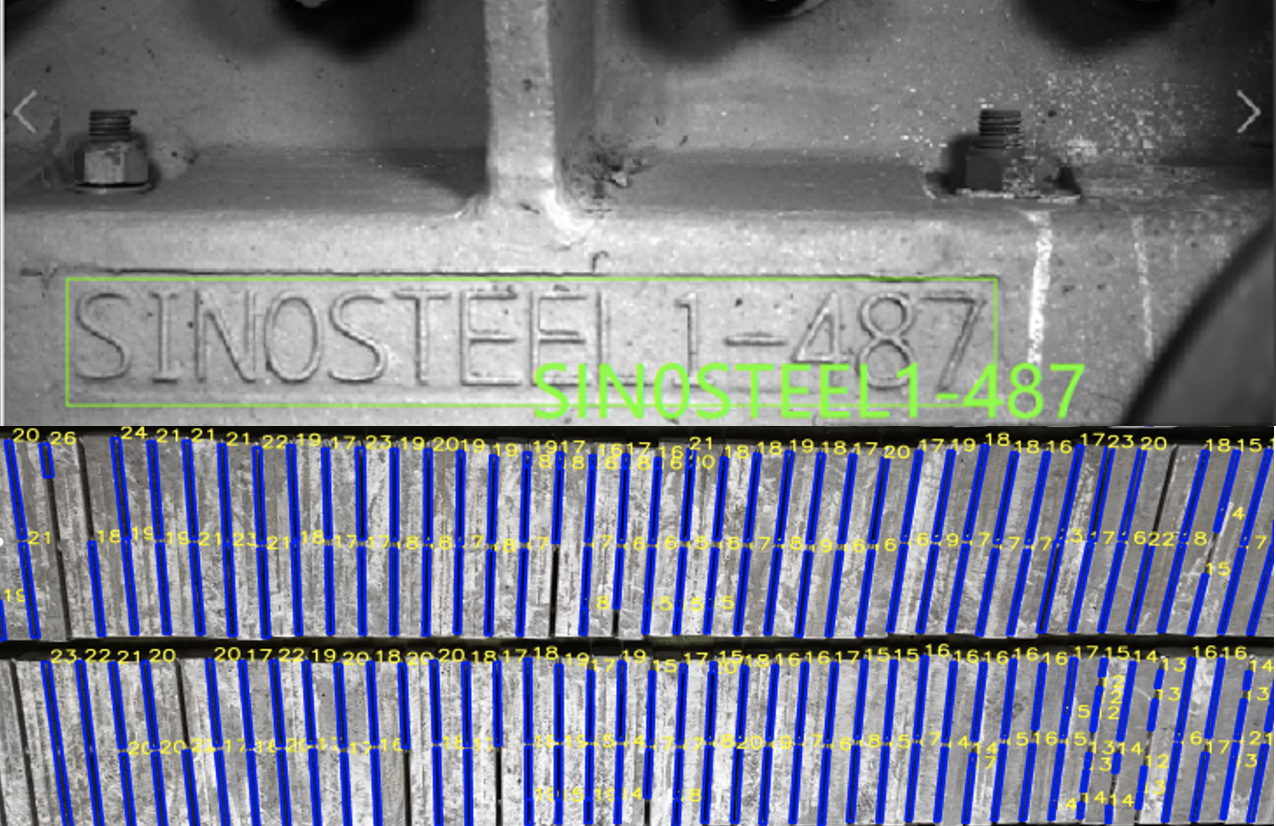
Image Recognition
Combining image recognition and machine learning algorithms with big data analysis and prediction technologies, the system realizes identification of operating status, defects, faults as well as full life cycle management of traveling grate trolleys.
Adopting image recognition algorithms, the system identifies trolley numbers and grate bar images to realize trolley positioning and tracking, calculates the gap width between grate bars and monitors equipment status in real time. Combined with data of wheels, beam deflection, side plates and other information, it evaluates the remaining service life of trolleys and implements life cycle management. Predicting and preventing equipment faults effectively safeguards stable production.
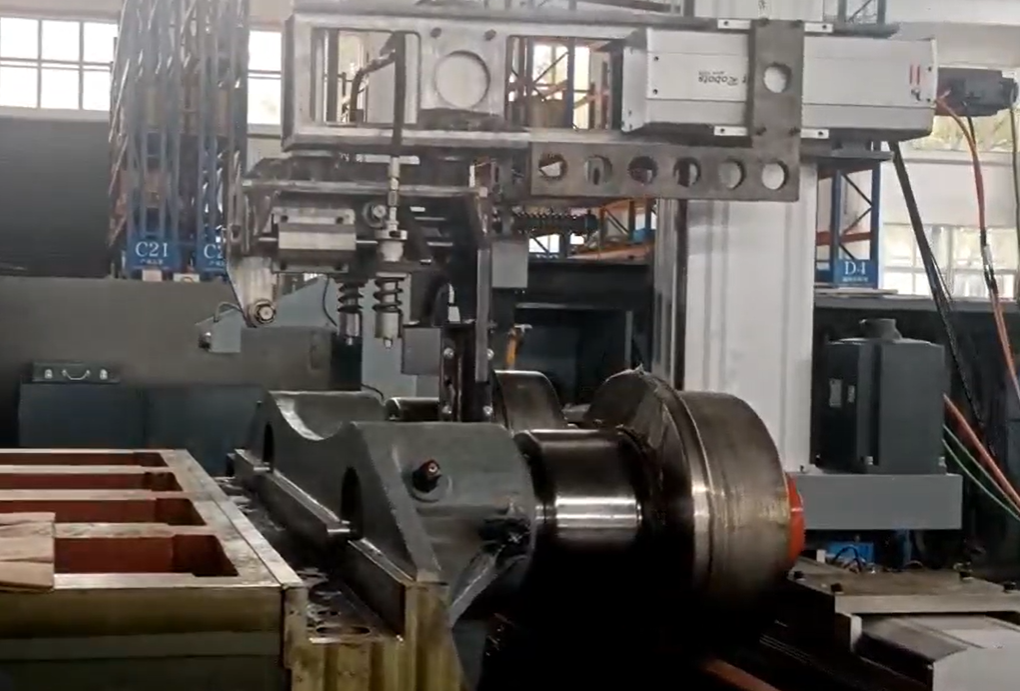
Automatic Oil Injection Device
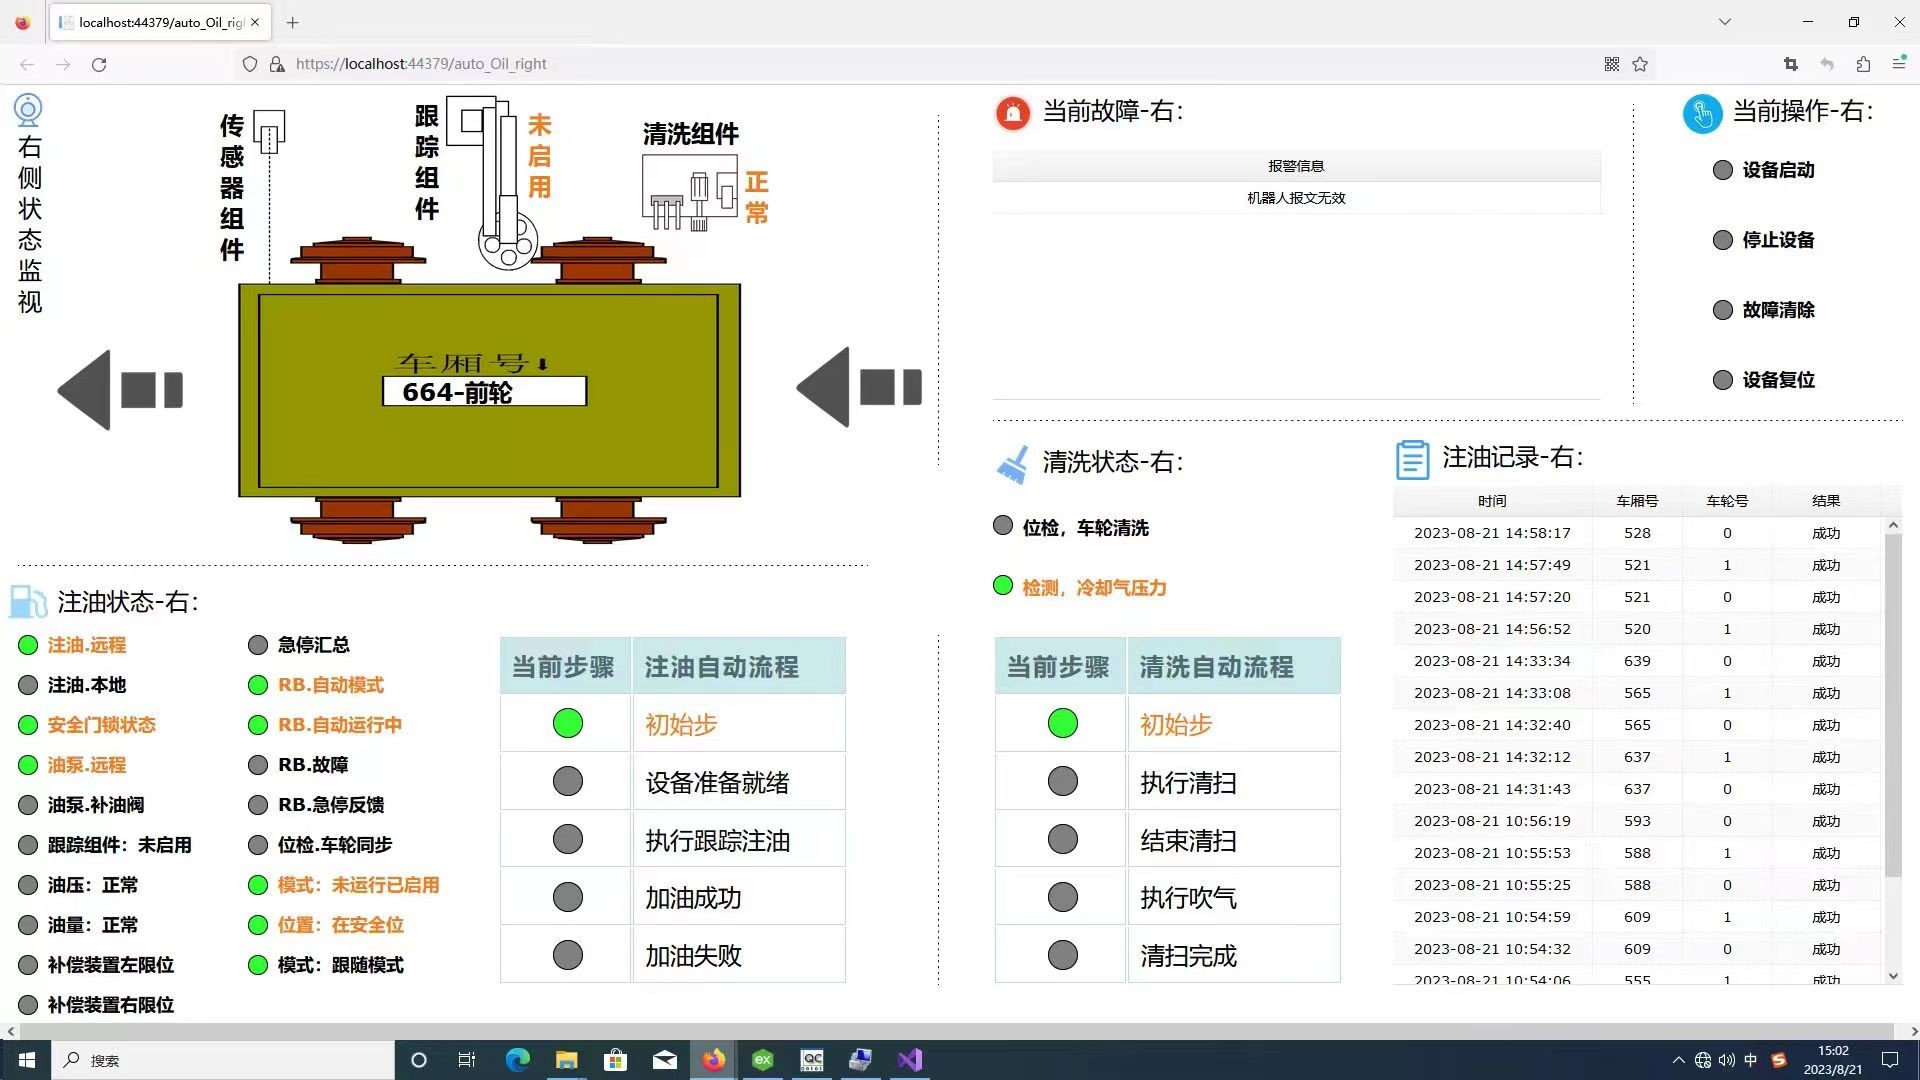
Trolley Automatic Lubrication System
According to the lubrication cycle requirements of traveling grate trolley wheels, machine vision technology is used to locate trolley wheels and calculate their operating speed for coordinated control via control modules. The module ensures synchronous movement between the oil injection mechanism and wheels during lubrication. Flexible design of oil supply connectors avoids damage to grease nipples. The system realizes follow-up automatic oil injection for trolley wheels to maintain reliable lubrication performance.
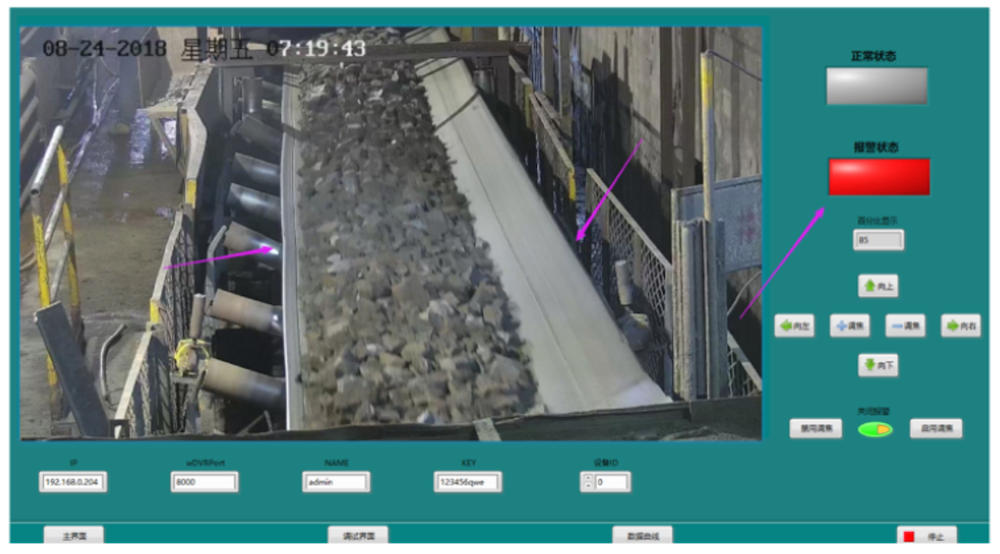
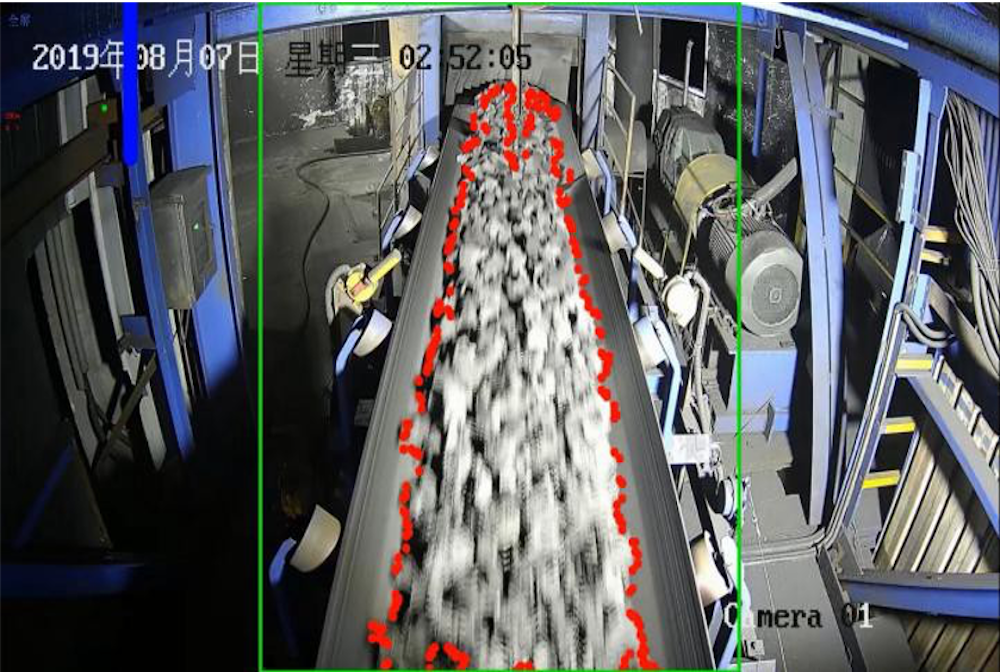
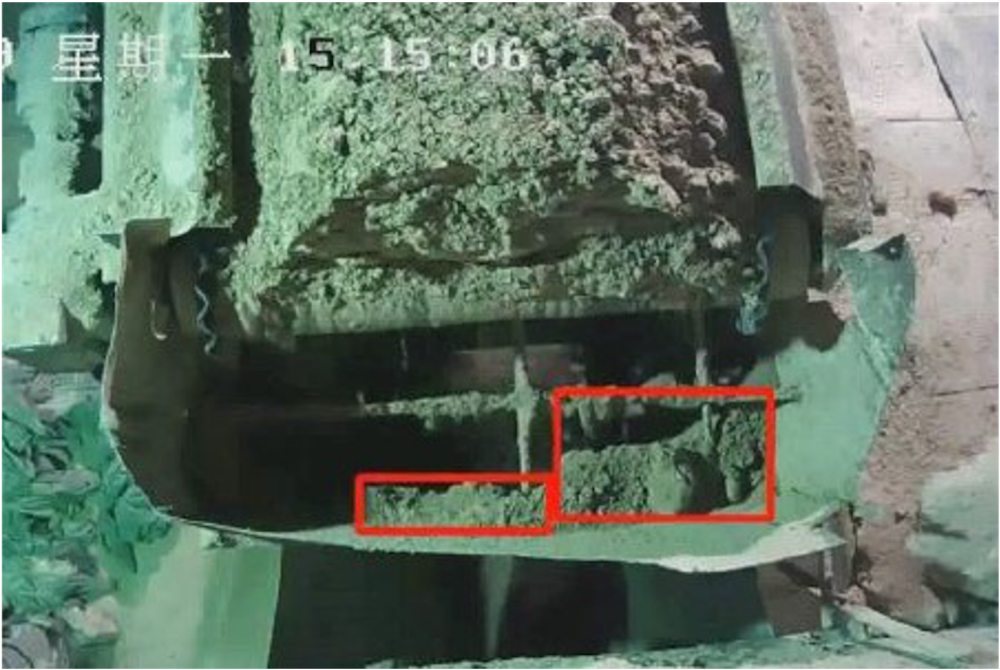
Supported by online equipment monitoring and predictive fault diagnosis system together with multiple intelligent automatic devices, the system addresses common pain points including belt deviation, tearing, slipping, material blockage and heavy manual inspection workload, realizing low-labor operation of the belt conveying system.

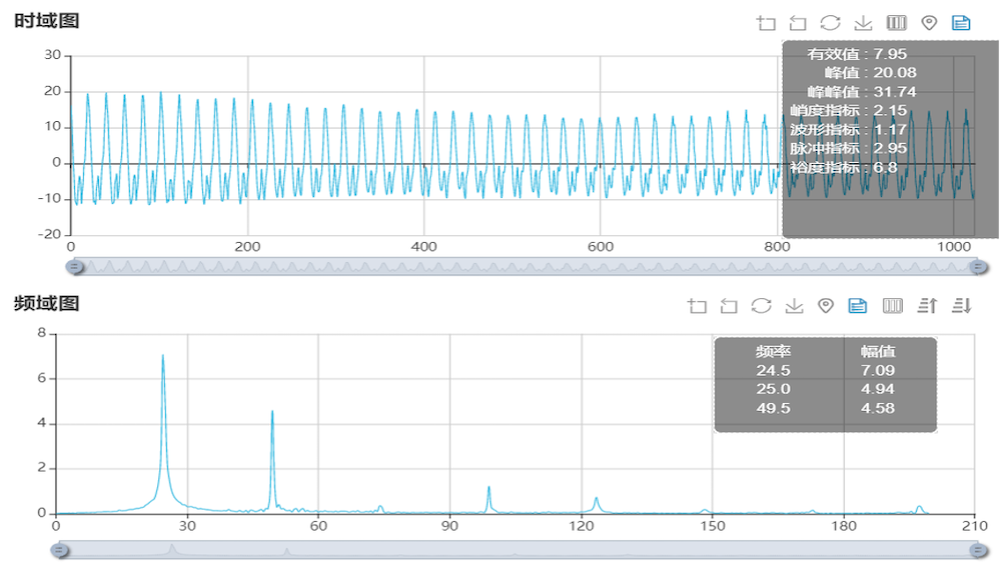
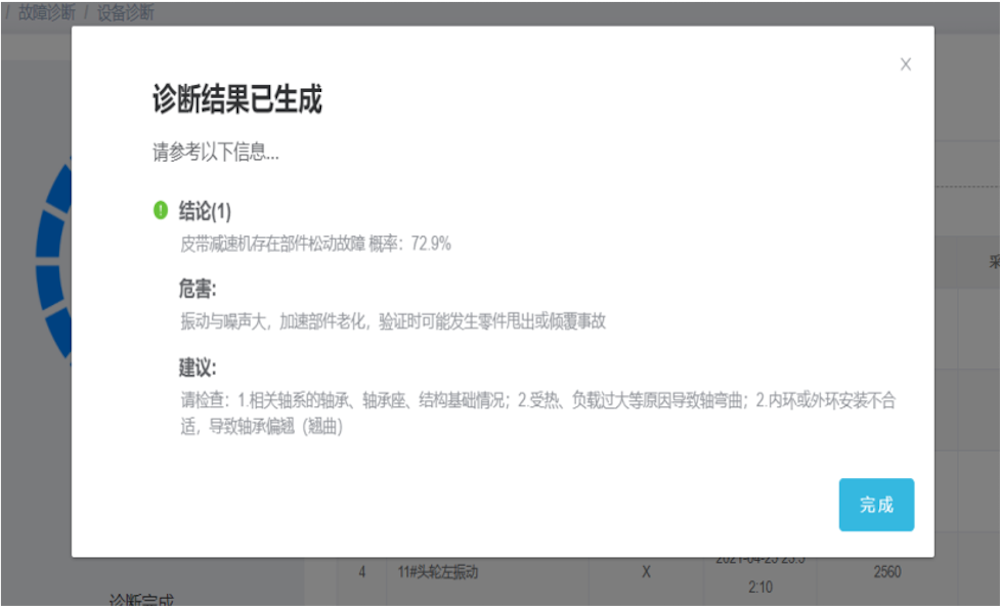
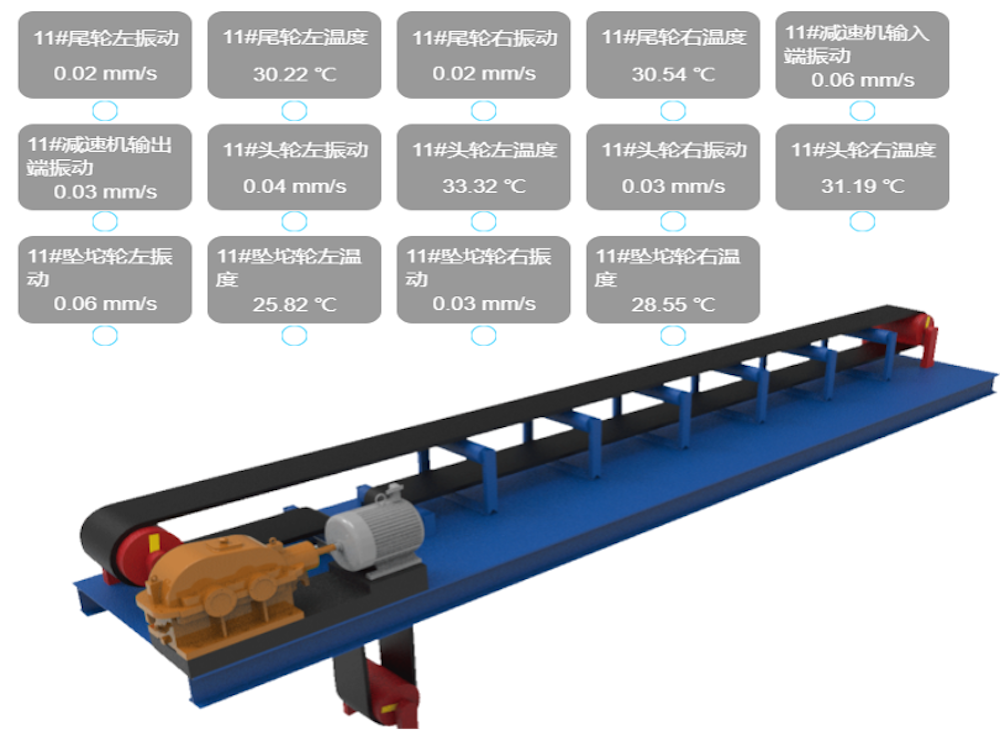
Intelligent sensors are installed on motors, reducers, head and tail pulleys of belt conveyor driving units and connected to the intelligent online monitoring & analysis platform. It realizes real-time online monitoring, operating condition analysis, intelligent fault diagnosis and predictive maintenance of belt conveyors.

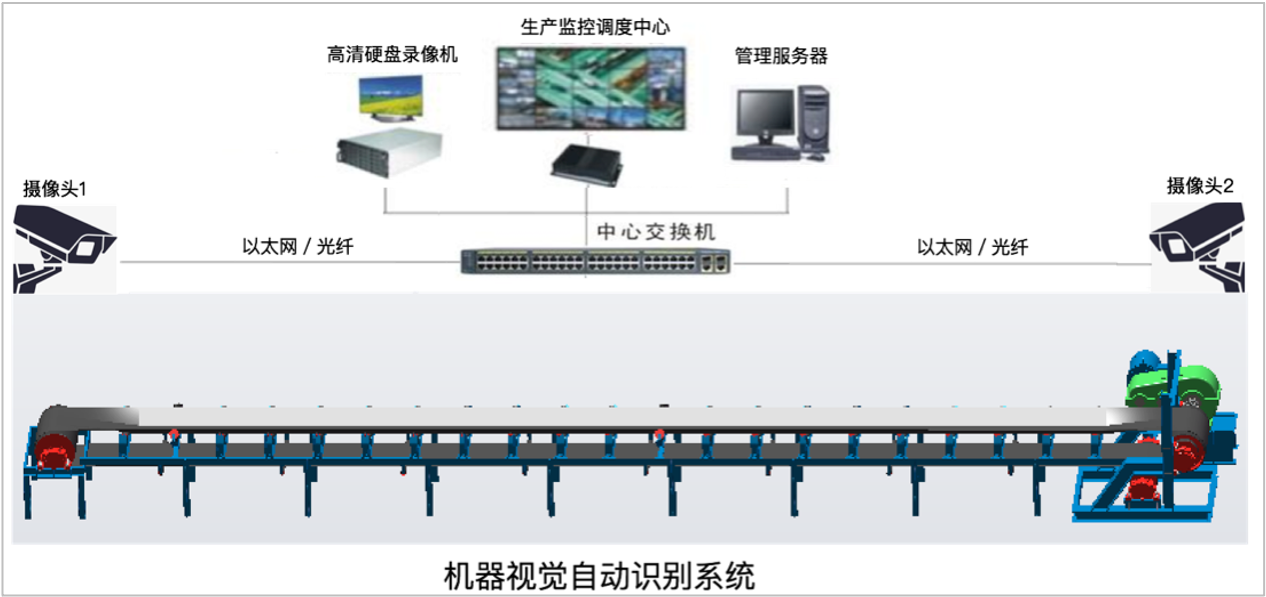
Monitoring cameras are arranged above conveyor galleries and key positions including conveyor head, tail and material drop points. High-definition images are transmitted to the machine vision server for processing and feature extraction. Intelligent image analysis algorithms automatically identify various abnormal operating conditions of the conveyor belt.
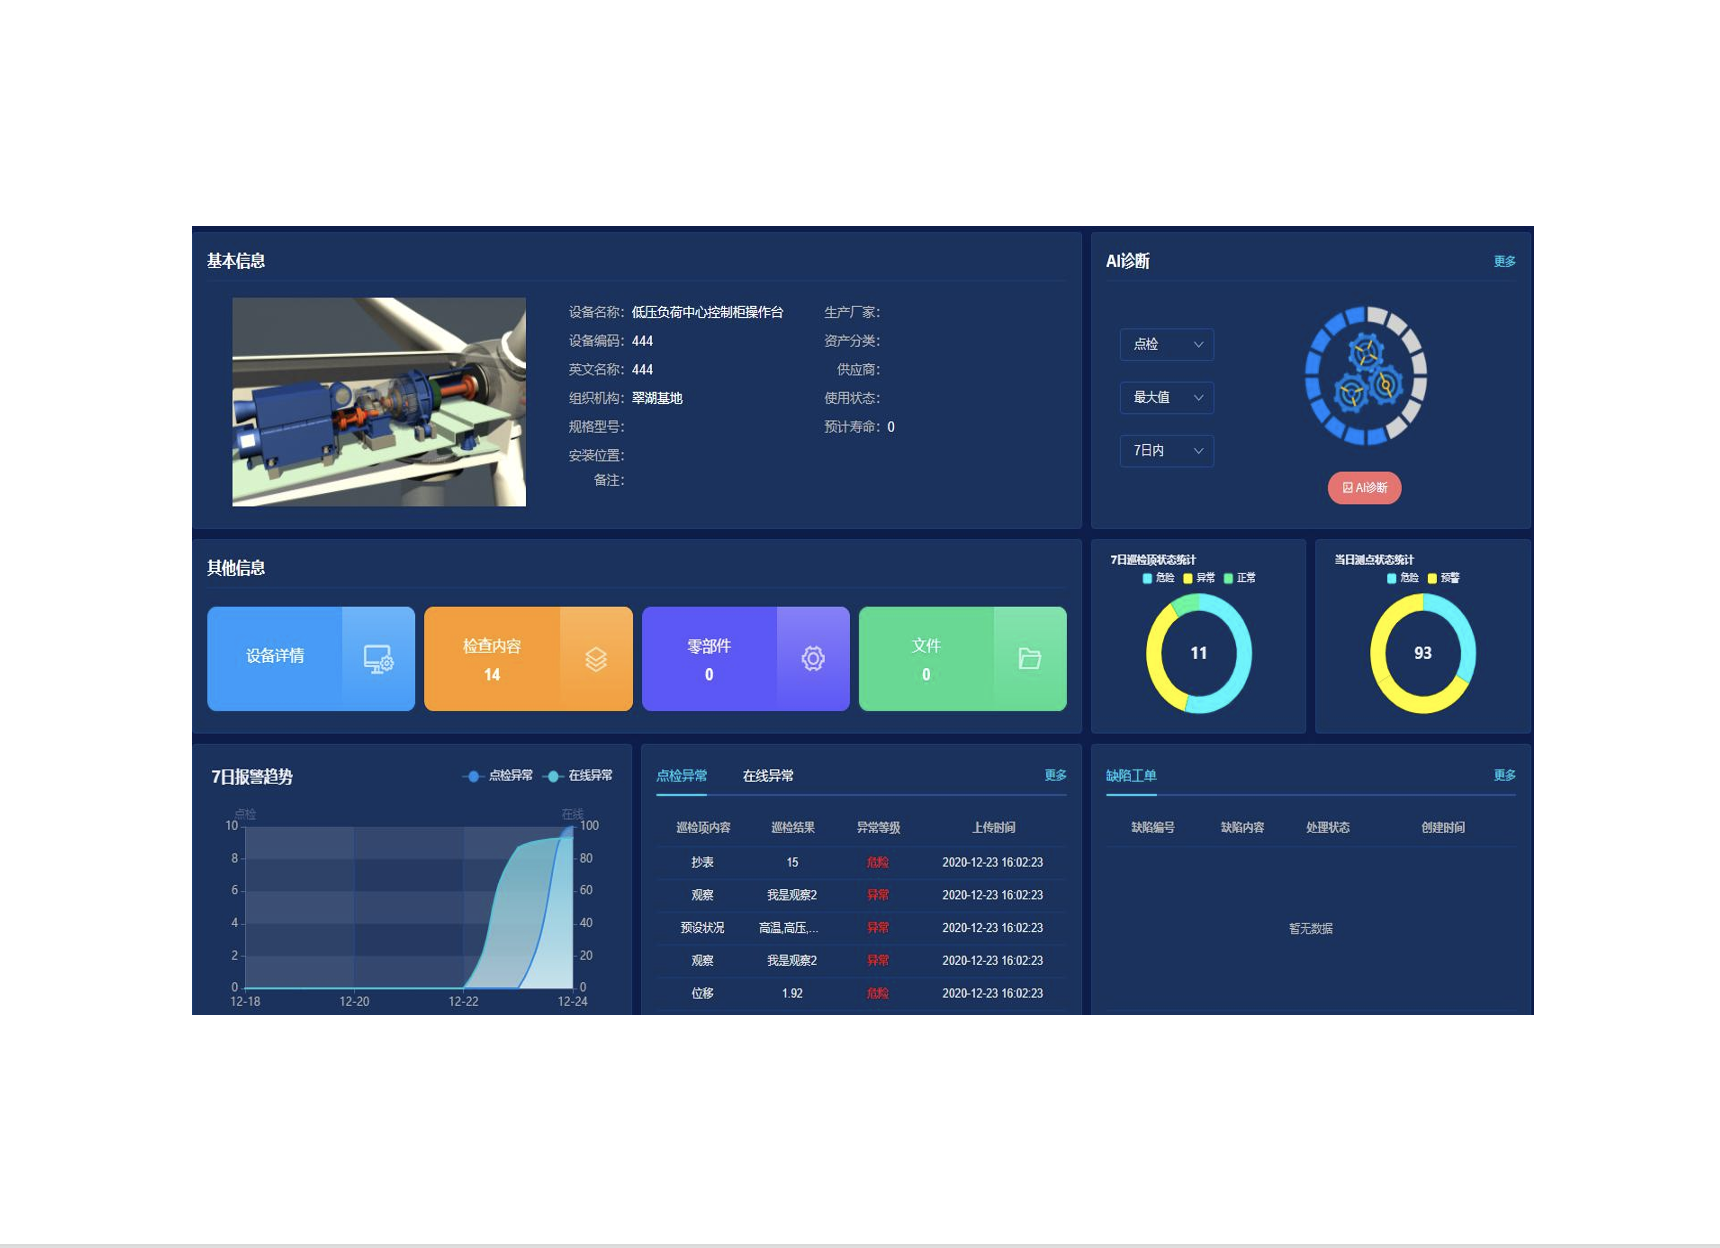
设备监测看板
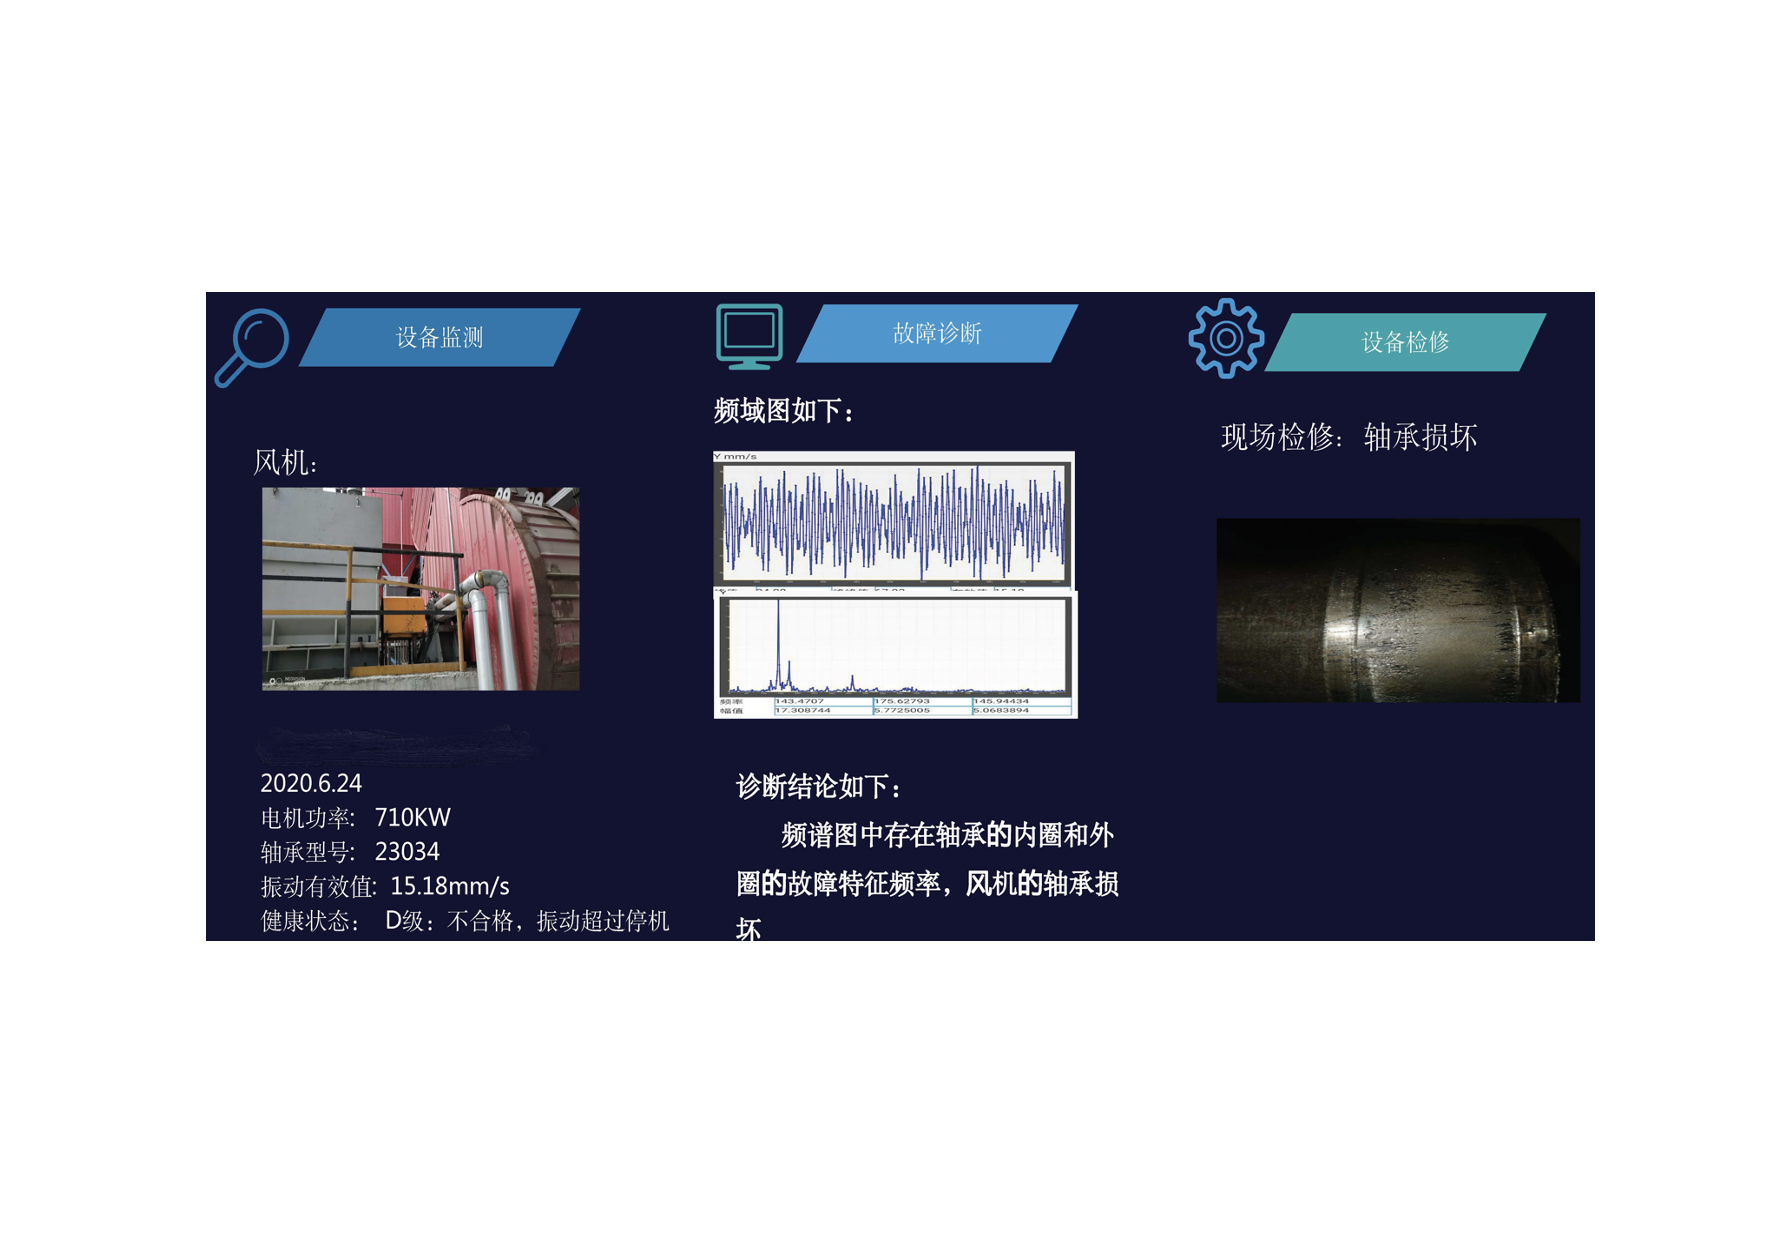
设备监测与预测性维护
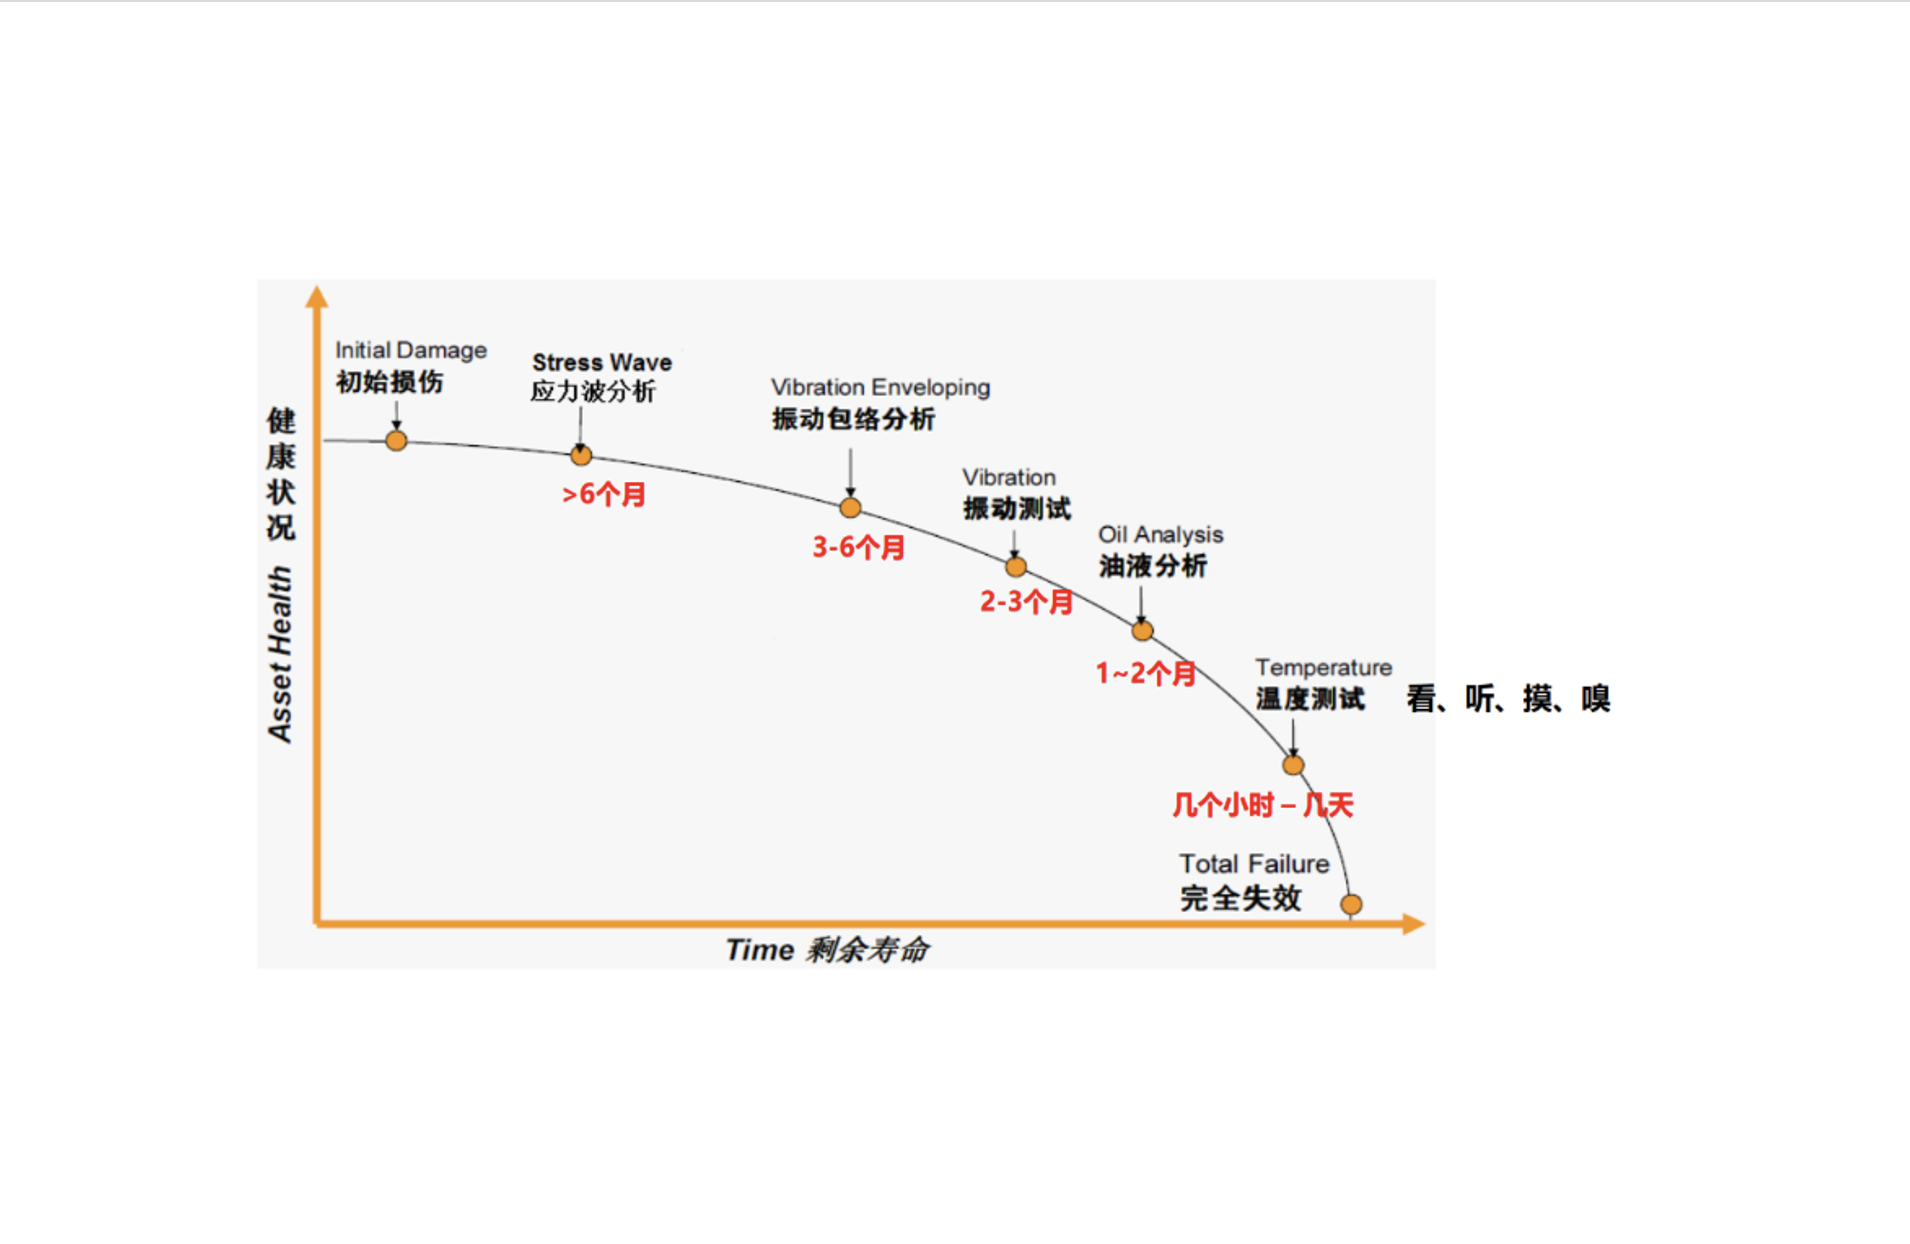
预测性维护
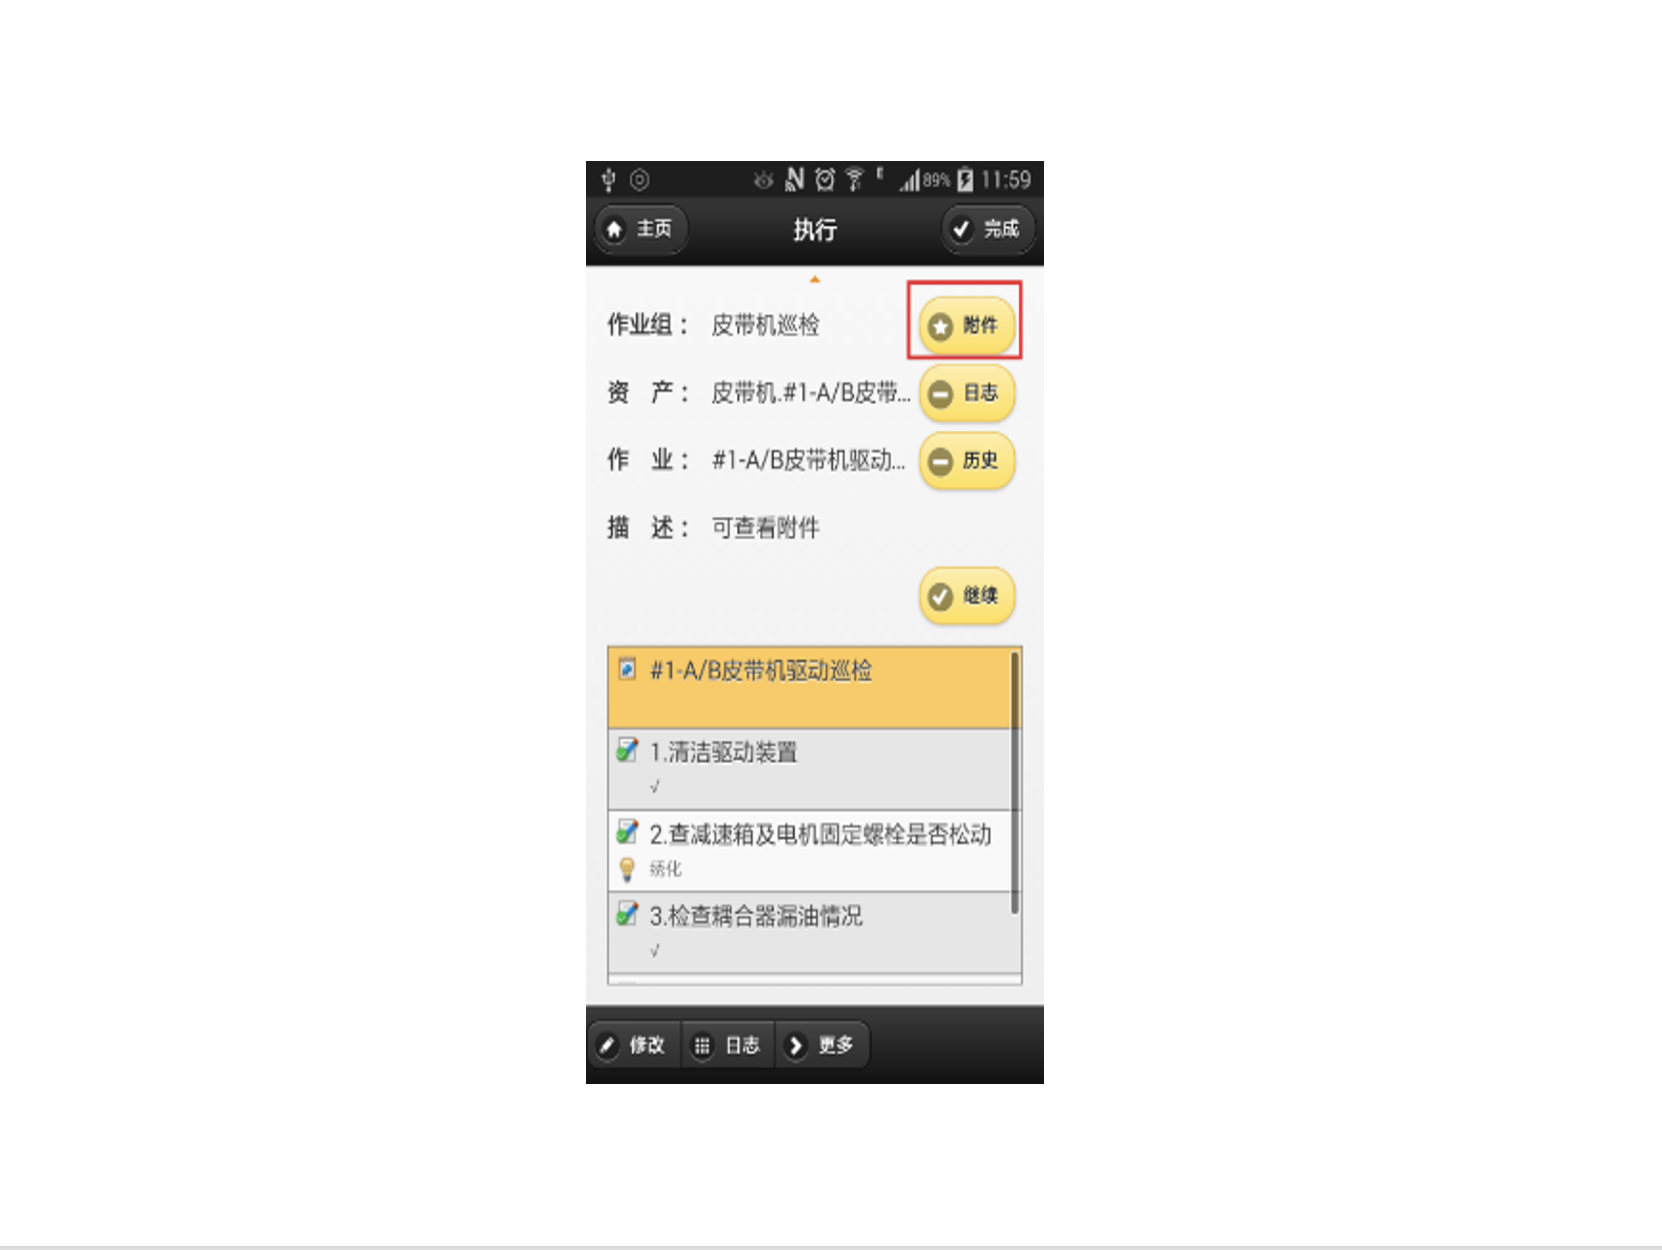
点巡检管理
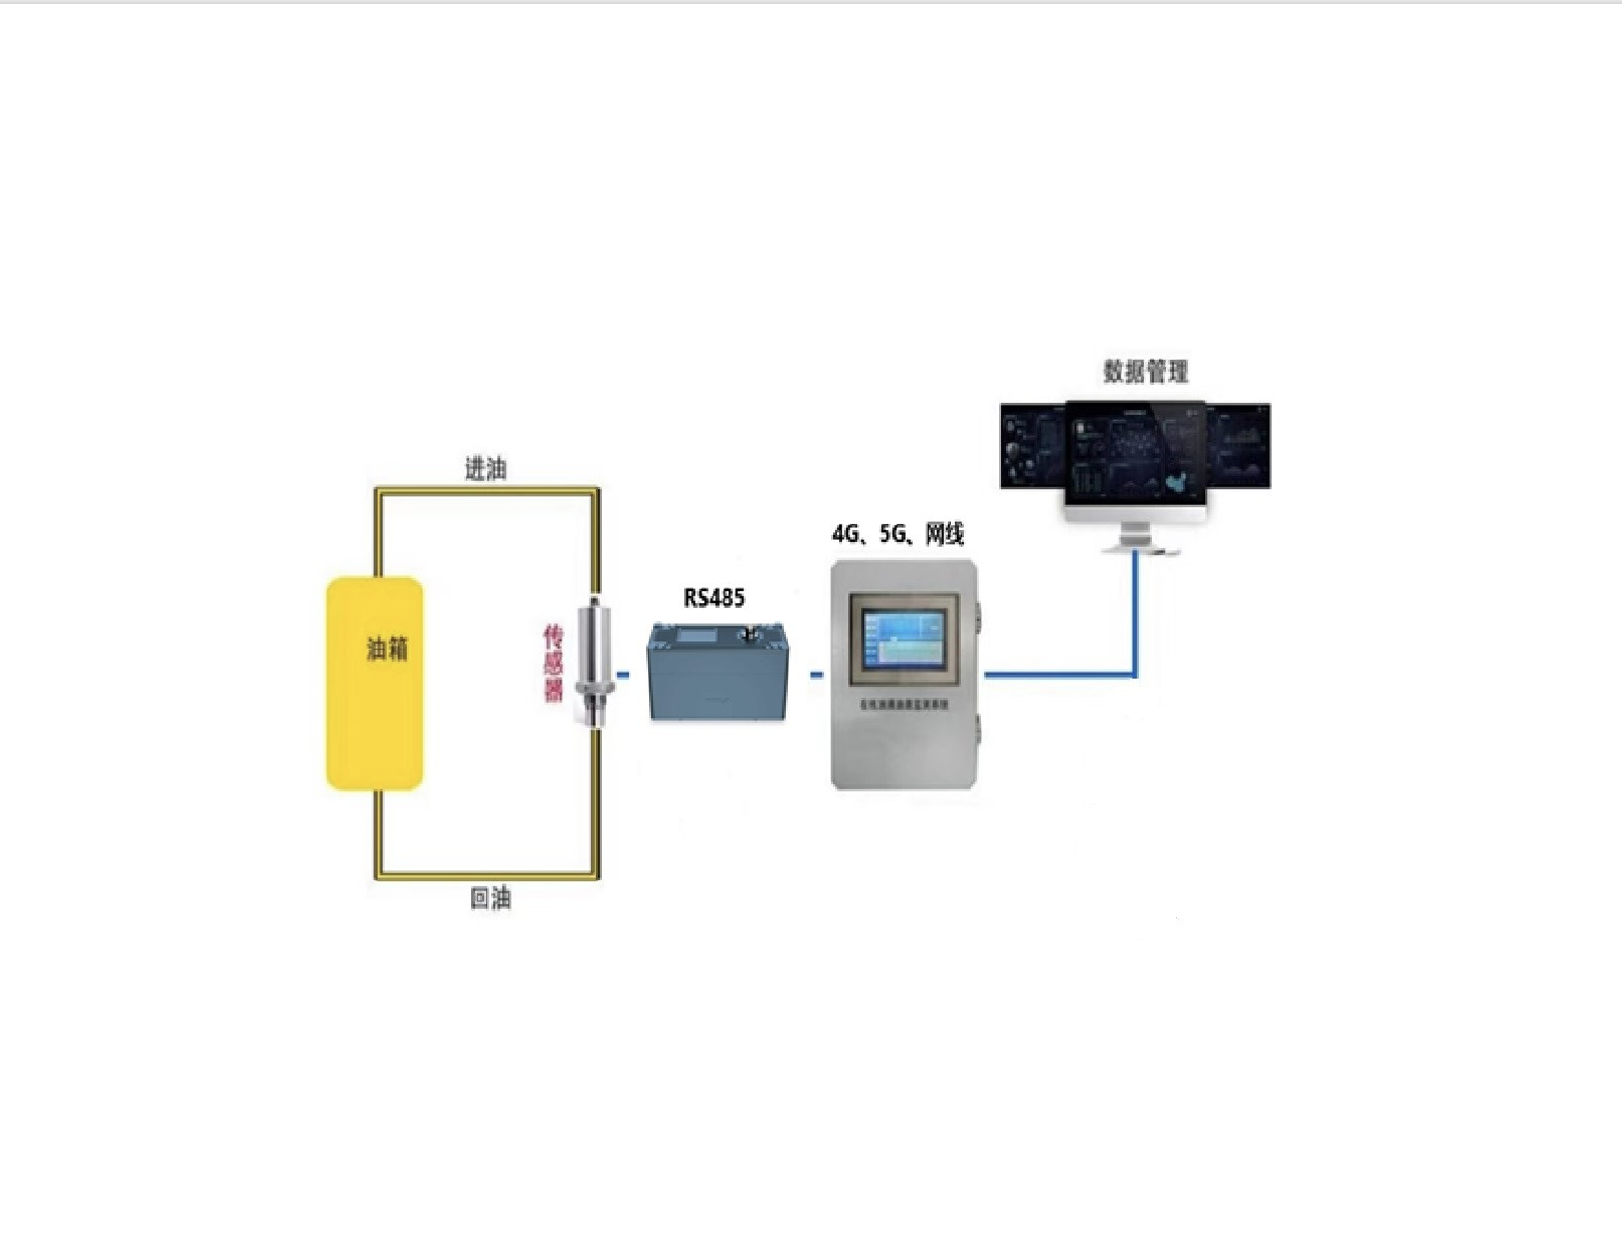
在线油液监测
Supported by big data, cloud service and Internet of Things technologies, a dynamic monitoring, fault early warning and predictive diagnosis platform is built for key transmission equipment. The system consists of the following modules:
Integrated equipment management dashboard
Online equipment monitoring and predictive maintenance
Online lubricating oil monitoring
Mobile APP inspection management
Copyright © China Grand Union Technology Co.,Ltd.(CGUTEC) All Rights Reserved. 京ICP备2021005877号-1